Choosing the right carriage bolt is not a cosmetic decision. It affects joint strength, installation speed, corrosion resistance, and long-term maintenance.
Industry standards provide a useful starting point. ASME B18.5 defines key dimensions for round-head square-neck bolts, including head size, neck geometry, and length tolerances. ASTM F3125 and ASTM A307 also show why material grade must match the application, although neither standard automatically makes every bolt suitable for structural use. The American Iron and Steel Institute’s Steel Construction Manual emphasizes verified material properties and traceability. These details matter when a bolt sits inside a timber frame, trailer bracket, or outdoor steel assembly.
A High Quality Carriage Bolt should have a clean, well-formed square neck. The neck must bite firmly into the receiving material without excessive hammering. Inspect the threads under bright light. They should appear continuous, sharp, and free from flattened sections. Check the head for cracks, deep dents, and uneven plating. Small defects can become serious after repeated vibration.
Market research from Grand View Research identifies construction, automotive, and machinery as major fastener demand sectors. That demand can encourage low-cost substitutions. Cheap is not always efficient. A box may look acceptable while containing mixed grades or inconsistent dimensions.
The selection process is not perfect. Even experienced buyers can overlook packaging errors. Confirm the manufacturer’s test certificates, coating specification, diameter, length, and applicable standard. Then test a sample in the actual material. A bolt that installs smoothly, clamps evenly, and resists visible corrosion is more trustworthy than one chosen by appearance alone.
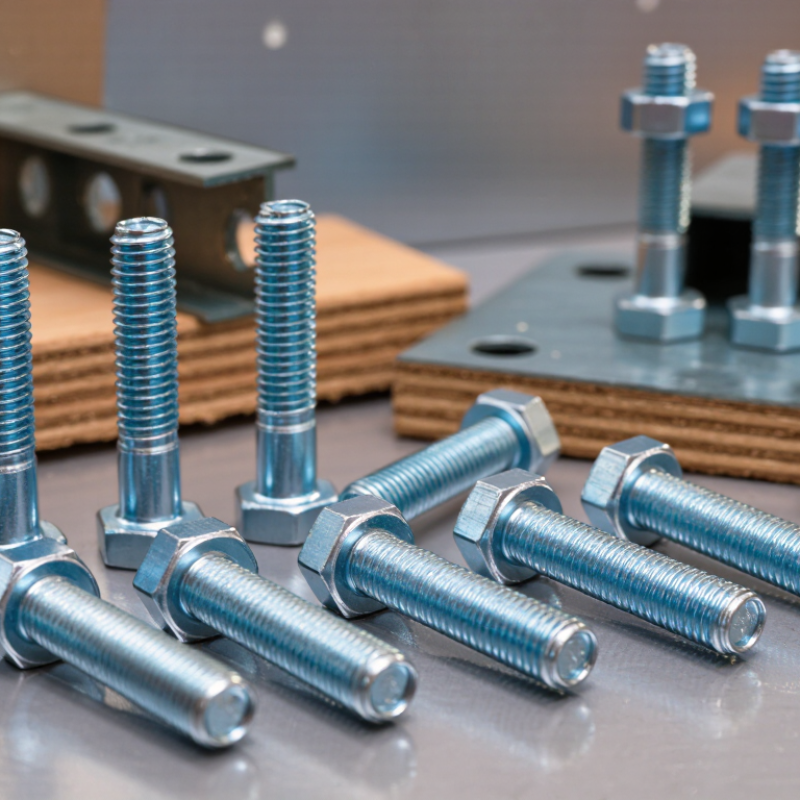
A high-quality carriage bolt starts with the correct type, not just a shiny finish. ASME B18.5 defines dimensional requirements for inch-series carriage bolts. These requirements cover head shape, head diameter, neck dimensions, bolt length, and dimensional tolerances. The common round head with a square neck suits timber and metal assemblies. The neck locks into a prepared hole while the nut is tightened. Short-neck, fin-neck, and rib-neck designs serve different grip conditions. Selection should match the material thickness and hole geometry.
Size decisions need more care than choosing a familiar diameter. Measure the clamped materials before selecting the bolt length. The threaded portion must engage the nut fully without excessive projection. ASME B18.5 tables help verify diameter, length range, head dimensions, and neck details. Thread designation matters too. A coarse thread often performs well in general structural assembly, but the drawing or engineering specification should control. Do not assume every carriage bolt follows the same thread series.
Look closely at the bearing surface and square neck. Uneven forming, damaged threads, or a tilted head can signal poor production control. Check the material grade and coating separately, because ASME B18.5 mainly addresses dimensions. Supplier inspection records should identify the standard, size, material, and batch. A clean certificate helps, but it is not a substitute for sample measurement. In field work, small errors appear quickly. A bolt that fits the hole may still fail the design requirement. Recheck the washer, nut, torque method, and actual load before approval.
Choosing a carriage bolt starts with tensile strength, not appearance. SAE J429 lists Grade 2 at 60 ksi minimum tensile strength, Grade 5 at 120 ksi, and Grade 8 at 150 ksi. These values describe the bolt’s resistance to pulling forces. They do not guarantee better performance in every assembly.
Grade 2 suits light-duty applications with modest clamping loads. Grade 5 offers a practical middle range for equipment frames, brackets, and general structural connections. Grade 8 provides the highest tensile capacity in this group, but it demands correct tightening and compatible mating materials. According to SAE J429, approximate proof loads are 55, 85, and 120 ksi for Grades 2, 5, and 8. Proof load matters because it indicates stress before permanent deformation.
Do not choose Grade 8 automatically. That shortcut can fail. A carriage bolt with a thin square neck may lose holding power if the hole is oversized or the material compresses. Test procedures under ASTM F606/F606M also show why controlled tensile testing matters; actual results depend on diameter, thread condition, heat treatment, and sampling. I would verify the grade mark, diameter, grip length, and washer fit before installation. Strength data is useful, but field conditions are less tidy. Corrosion, vibration, and uneven tightening still deserve attention.
| Comparison Dimension | SAE J429 Grade 2 | SAE J429 Grade 5 | SAE J429 Grade 8 | Selection Guidance |
|---|---|---|---|---|
| Minimum tensile strength | 74 ksi for 1/4–3/4 in. 60 ksi for >3/4–1-1/2 in. |
120 ksi for 1/4–1 in. 105 ksi for >1–1-1/2 in. |
150 ksi for 1/4–1-1/2 in. | Choose a higher grade when the joint is exposed to greater tensile, shear, vibration, or fatigue loads. |
| Approximate tensile strength | 60–74 ksi | 105–120 ksi | 150 ksi | Do not compare grades without checking the nominal diameter, because the specified minimum can vary with size. |
| Typical SAE head marking | Usually unmarked | Three radial lines | Six radial lines | Use head markings as an initial identification check, then confirm the product certificate or applicable specification. |
| Typical hardness range | Approximately Rockwell B69–B100 | Approximately Rockwell B80–C34 | Approximately Rockwell C24–C38 | Hardness is a supporting quality indicator; it does not replace tensile or dimensional verification. |
| Suitable load level | Light-duty | Medium- to heavy-duty | High-load and demanding service | Select the lowest grade that safely meets the engineered joint requirements; higher strength is not automatically better for every assembly. |
| Common carriage-bolt uses | Wood framing, light brackets, general maintenance | Equipment frames, trailers, structural brackets | Heavy machinery, high-load connections, vibration-prone assemblies | Confirm that the selected carriage bolt has the required neck, head, thread, and dimensional configuration. |
| Corrosion protection | Often available plain or zinc-plated | Often available plain, zinc-plated, or coated | Often supplied plain or with a compatible protective coating | Select the coating separately from the strength grade and verify hydrogen-embrittlement controls for high-strength plated fasteners. |
| Recommended inspection points | Thread condition, dimensions, surface defects, marking | Grade marking, dimensions, hardness, tensile certification | Grade marking, hardness, tensile certification, coating condition | For critical applications, request material and mechanical-property documentation and inspect samples against the purchase specification. |
How to Choose High Quality Carriage Bolts?
High quality carriage bolts begin with verified dimensions, not a polished surface. ASME B18.5 provides dimensional and tolerance guidance for round head square neck bolts. Measure the bolt diameter, length under the head, head diameter, and neck height. A digital caliper helps reveal small deviations. The square neck must seat firmly without damaging the mounting hole.
Thread fit deserves equal attention. Confirm the thread diameter, pitch, and series before ordering nuts or threaded inserts. A matching nut should run smoothly by hand across the usable thread. It should not wobble, bind, or stop early. A thread pitch gauge can identify mistakes that visual inspection misses. Avoid forcing a nut with a wrench during inspection. That action can hide poor thread quality.
In receiving inspections, compare several samples rather than checking one bolt. Check the thread with a suitable go/no-go gauge when available. Examine the bearing surface for dents, folds, or uneven forming. These defects may reduce clamping reliability. Coating thickness can also affect thread fit, especially near the first thread. A clean appearance can mislead me. I once treated uniform color as proof of quality, but dimensional checks showed otherwise. Tolerances matter more than shine. Keep inspection records with measured values, gauge details, and lot information. This makes supplier discussions clearer and supports consistent installation decisions.
How to Choose High Quality Carriage Bolts?
A bright finish can look impressive, but appearance alone does not prove coating performance. ASTM B633 covers electrodeposited zinc coatings on iron and steel products. Request the specified service condition and minimum coating thickness. These details matter more than color. During receiving inspection, check the bolt head, square neck, threads, and recessed areas. Uneven coverage may hide beneath the head. A calibrated coating thickness gauge provides stronger evidence than visual inspection. Ask for lot-specific test records, not generic certificates. Small paperwork gaps can create large quality questions.
ASTM B117 evaluates corrosion resistance through a controlled salt spray test. It does not predict exact outdoor service life. A bolt lasting 500 hours in salt spray will not automatically last 500 hours outside. Define the failure point clearly, such as white corrosion or red rust. Also confirm the test duration, sample quantity, and inspection method. Threaded areas deserve attention because damage during handling can expose steel. I have found that buyers sometimes compare test hours without comparing coating thickness. That comparison is incomplete.
Tips: Measure coating thickness on several locations. Inspect threads under magnification. Confirm the B633 service condition. Treat B117 hours as comparative data, not a guarantee. When results seem perfect, investigate further.
Zinc coating thickness requirements for carriage bolts under ASTM B633 service-condition classifications
The chart shows the minimum zinc coating thickness commonly specified for ASTM B633 service conditions: SC1 = 5 μm, SC2 = 8 μm, SC3 = 12 μm, and SC4 = 25 μm. A thicker coating generally provides greater protection when the bolt is exposed to moisture or corrosive environments. ASTM B117 defines a neutral salt-spray test method, but it does not establish one universal pass/fail exposure time for all zinc-coated carriage bolts; acceptance criteria must be agreed in the product specification.
Reference: ASTM B633, Standard Specification for Electrodeposited Coatings of Zinc on Iron and Steel; ASTM B117, Standard Practice for Operating Salt Spray (Fog) Apparatus.
Before purchasing carriage bolts, verify the inspection records, not just the surface finish. A reliable supplier should provide dimensional reports for head diameter, shank length, thread size, and square-neck fit. Check the actual lot number. It must match the packaging, inspection report, and certificate. In receiving inspections, this simple comparison often reveals mixed batches. Small errors matter.
Traceability should follow each bolt from raw material to final packing. Request the heat number, production date, test batch, and inspection operator’s identification. The material certificate should state chemical composition and mechanical results, such as tensile strength and hardness. Confirm that testing followed the applicable standard or purchase specification. A certificate alone is not proof. It may contain copied data or unclear revisions. Ask questions when details feel vague.
Tips: Request samples before bulk delivery. Measure several bolts with calibrated tools. Check thread quality, coating uniformity, and square-neck engagement. For critical assemblies, use an independent laboratory to verify material and mechanical properties. Keep photos, reports, and shipment records together. This creates a practical audit trail. Do not rely on appearance alone. A bright finish can hide poor steel or incorrect heat treatment. I have seen documentation look complete while the lot number was missing. That weakness should stop approval until corrected.